Pipe offset calculator
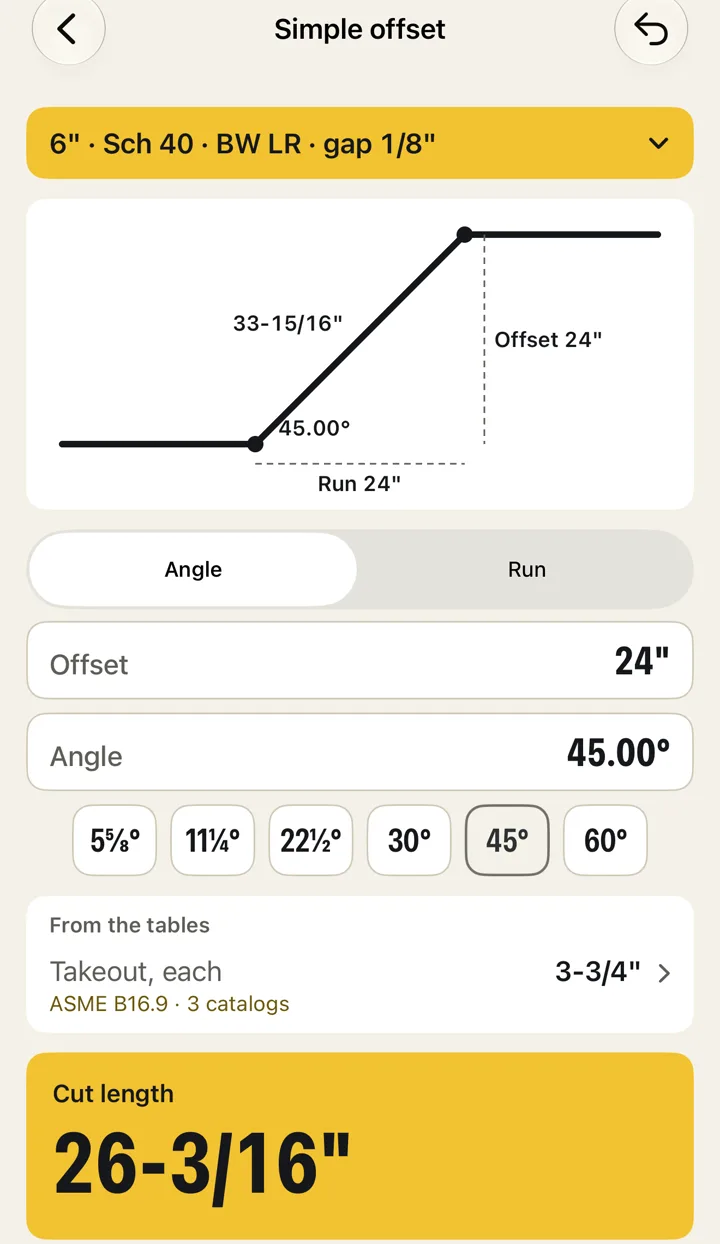
Two elbows move the line over by the offset. Enter the offset and the angle or the run; the cut length takes off both elbows and a weld gap at each end.
- Travel
- 33-15/16"
- Run
- 24"
- Angle
- 45.00°
- Takeout, each
- 3-3/4"
- ASME B16.9 · 3 catalogs
Mark the 90 before cutting it to the angle
Steps
- Travel = 24 × 1.4142 = 33.941"
- Run = 24 × 1.0000 = 24"
- Takeout = 3.75" eachASME B16.9 · 3 catalogs
- Cut = 33.941 − 2 × 3.75 − 2 × 0.125 = 26.191" → 26-3/16"
Verify critical dimensions against the current standard before fabrication.
A worked example
A 10" offset with a 12" run, on 6" pipe with long-radius 90s cut to the angle, and no gap. This one is from the worked examples in a handheld pipe calculator's published guide; the calculator here gives the same answers.
- Travel = √(10² + 12²) = 15.62"
- Angle = atan(offset ÷ run) = atan(10 ÷ 12) = 39.81°
- Takeout = R × tan(θ/2) = 9 × 0.3620 = 3.258" eachR: ASME B16.9 · 3 catalogs
- Cut = 15.62 − 2 × 3.258 = 9.104" → 9-1/8"
Before cutting each 90 to the angle, mark it along the inside 3-15/16", centerline 6-1/4", outside 8-9/16".
Cut the pipe to 9-1/8".
The same idea in millimeters
A 600 mm offset at 45°, DN 150 long-radius 45s, a 3 mm gap:
- Travel = 600 × 1.4142 = 848.5 mm
- Run = 600 × 1.0000 = 600 mm
- Takeout = 95.3 mm eachASME B16.9 · 3 catalogs
- Cut = 848.5 − 2 × 95.3 − 2 × 3 = 652 mm
The formulas
- Travel = offset ÷ sin θ and run = offset ÷ tan θ, θ being the fitting angle.
- With the run known instead: travel = √(offset² + run²) and θ = atan(offset ÷ run).
- Cut = travel − 2 × takeout − 2 × gap for butt welds: one takeout and one root gap at each end.
- A 90 cut to θ: takeout = A × tan(θ/2), where A is the 90's center to end.
| Angle | Travel = offset × | Run = offset × | Takeout of a 90 cut to it = A × |
|---|---|---|---|
| 5-5/8° | 10.2023 | 10.1532 | 0.0491 |
| 11-1/4° | 5.1258 | 5.0273 | 0.0985 |
| 22-1/2° | 2.6131 | 2.4142 | 0.1989 |
| 30° | 2.0000 | 1.7321 | 0.2679 |
| 45° | 1.4142 | 1.0000 | 0.4142 |
| 60° | 1.1547 | 0.5774 | 0.5774 |
Questions
Travel or cut length?
Travel is center to center between the two elbows. The cut length is the pipe you cut: the travel less both takeouts and a gap at each weld.
Which takeout does it use?
For long-radius elbows at 45°, the stock 45 from the elbow takeout chart. At any other angle, a 90 cut to the angle: A × tan(θ/2). Short-radius elbows don't come as stock 45s in the chart, so they're cut from a 90 too. For socket-weld, threaded, or a fitting you measured, open the pipe bar and choose My takeout.
Why two gaps?
The pipe has a weld at each end, and each weld has its own root gap. Set the gap to 0 for a fitting with no gap.
It says there's no pipe left to cut
The two elbows and gaps take up more than the travel. A bigger offset or a smaller angle gives a longer travel; a shorter fitting gives more pipe.
Can I work in metric?
Switch to mm. What you've typed converts, so 1/8" becomes 3.2 mm instead of resetting.
Where the takeouts come from
Elbow center-to-end values are ASME B16.9 dimensions that agree in at least two of these catalogs:
- Stainless steel butt weld fittings
- Product guide: pipe fittings & flanges (stainless)
- Weldbend catalog: fittings, flanges and technical data (2010 edition, current on weldbend.com)
Pipe outside diameters, used for the cut marks:
- Number and size of bolts for flanged joints (ASME B16.5) and pipe schedule chart
- Welded and seamless pipe dimensions and weights (hosted by Ferguson Industrial)
- Steel pipe specification sheets (Sch 40, 80, 160, XXH) and ASME B1.20.1 / B16.11 tolerance sheets
- Product catalog ver 5.1
- Weldbend catalog: fittings, flanges and technical data (2010 edition, current on weldbend.com)
Verify critical dimensions against the current standard before fabrication.
Keep it in your pocket
The app does this offline, saves it to a job and prints a cut sheet, and adds rolling offsets, laterals, miters, saddles and the fitting tables. $19.99 once, no subscription.
Coming soon to the App Store$19.99 once · iPhone and iPad